

The global manufacturing industry is undergoing a major transformation, marked by the adoption of automated technologies, increased efficiency and enhanced product quality.
Overall, the industry is moving away from reactive measures and toward proactive ones. Leveraging modern technology, manufacturers can act in a predictive manner, ensuring operations remain optimised and effective for longer periods of time than ever before.
Industry 4.0
Industry 4.0 is the next logical step in the development of manufacturing technologies. Put simply, it’s the marriage of information technology and manufacturing operations. This means automation, advanced robotics and machine-to-machine communication join together to boost productivity and efficiency, ultimately lowering overhead and strengthening the bottom line.
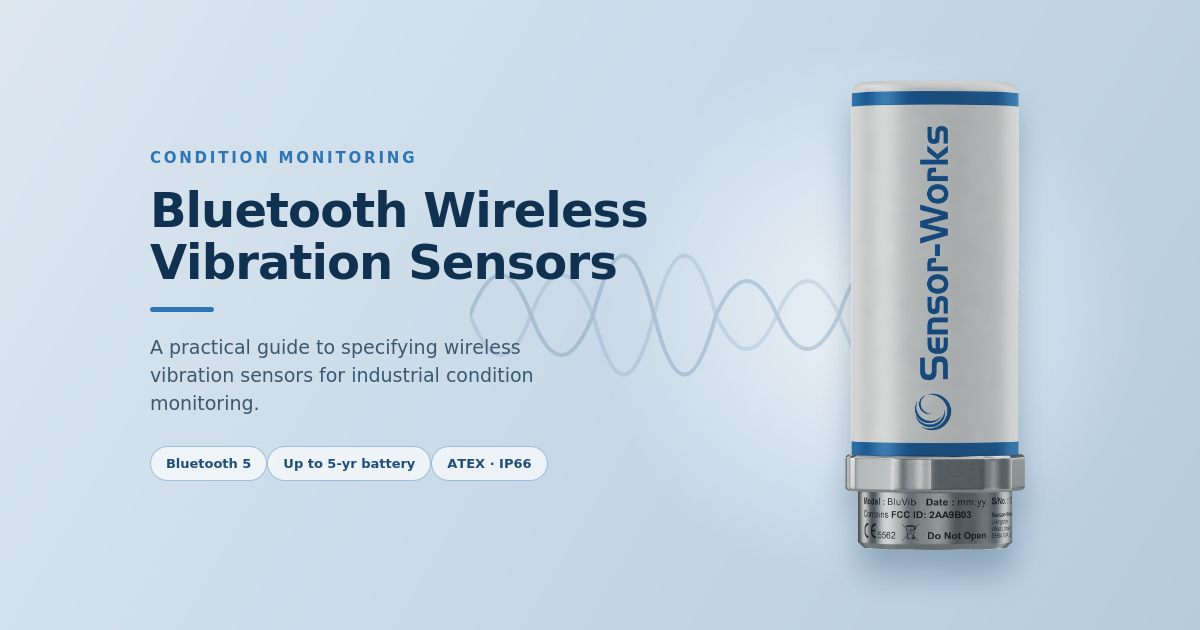
But Industry 4.0 goes well beyond automation alone. The factory devices that make up the bulk of the Industry 4.0 ecosystem aren’t just connected and communicative, they are “intelligent.” The equipment of the fourth industrial revolution use wireless sensors – either built-in or retrofitted – to capture, analyse and react to data from the environment surrounding them. This is where Big Data and Industry 4.0 synergise.
A report on the Internet of Things for industry estimates that Big Data and Industry 4.0 could add as much as £14.2 trillion to the world economy by 2030 through its ability to improve productivity, reduce operating costs and enhance product quality.
These are just some of the benefits manufacturers can expect:
- Increased competitiveness: Manufacturers previously turned to outsourcing to keep labour costs down and remain competitive. Industry 4.0 not only keeps labour costs low – smart, automated processes require less human operators – but also improves the efficiency of the process as a whole. The end result is a nimbler, more competitive enterprise.
- Increased productivity: Around-the-clock automation and deep, granular insights into the entirety of the manufacturing process ensures greater productivity. Empowered by machine learning algorithms, your factors of production can run better, for longer, at a lower cost and with less downtime disruptions.
- Better record-keeping and archiving: A byproduct of capturing and cataloguing vast troves of data is that manufacturers will have access to all the necessary information for internal operations, regulatory compliance and consumer facing transparency efforts.
- Improved business structures and business relations management: Collateral data also presents a big opportunity. Manufacturers can sell the information outright to market research and analysis firms looking to bolster data sets and strengthen their findings. Or, they can leverage the information uncovered to restructure agreements with their suppliers.
With smart manufacturing increasingly allowing generalised equipment structures to serve hyper-specialised functions, pushing more production responsibilities higher up the supply chain makes sense for all parties. It’s an opportunity for suppliers to increase their market share and value adds, while removing some of the capital burdens from smaller, later stage manufacturers and allowing them to focus on their core offering.
With data now ubiquitous across the supply chain, there’s also added scrutiny. This is another opportunity for shrewd business people to repackage and sell their internally developed know-how for external purposes.
IoT-empowering Industry 4.0
The vast achievements of the modern manufacturing plant – whether it’s more automation, predictive maintenance, increased efficiency, or enhanced product quality – almost always trace back to one tiny component: the sensor.
With this piece of technology, manufacturers gain insight into operational processes that may have been previously understood but are difficult to keep tabs on so long as nothing is majorly wrong. Drawing on the vast amount of data generated, wireless sensors enable smarter, more agile decision-making.
These sensors continuously collect and transmit granular data, which ultimately sheds light on the functionality of the larger system and allows for decision-makers to identify opportunities for improvement. Whether it’s detecting machine idling or issues like air leaks, sensors enable manufacturers to catch problems early on and correct them through maintenance, repairs or upgrades – before they impact productivity.
The ultimate goal, of course, is optimised production. Bringing together the benefits of the Internet of Things, Big Data and Industry 4.0 ensures greater uptime. Planned and unplanned maintenance can occur on a predictive basis, ensuring that maintenance work will always and only be conducted when it is needed and at the time of least disruption to the operation.
Similarly, breakdowns can be made a thing of the past and the factory floor can be turned into a symphony of perfectly orchestrated movements. Assets, of course, will still need to be pulled offline for maintenance or decommissioning, but production will never halt.
In short, combining the forces of IoT, Big Data and Industry 4.0 will maximise ROI and optimise the efficiency of your manufacturing process. It’s all about the smart, connected systems that respond to real-world conditions and developments. Bringing next-generation connectivity, synchronicity and intelligence to manufacturing operations is driving better processes, quicker fixes and higher quality products – and at a lower cost to boot.